16. 4) M – Manufacturing Breadth
M · Manufacturing Breadth = “What kinds of things can we make here, to production quality?” (capability & depth)
Manufacturing Breadth is the means of making means. Mining to materials to machine tools to precision to electronics repair and “useful-node” semiconductors. What moves it is bootstrapping with measurement first, not machinery first. Proof lives in first-pass yield, calibration stability, and repair cycle times that fall quarter after quarter. Failure is QA theater: glossy work instructions, no scrap audits, and gauges that drift.
Quick Heuristic: M and A (Autarky) are often confused. Consider “Kitchen vs groceries”. M is the kitchen: tools, techniques, and the chef’s skill. A is how much of tonight’s menu you sourced from your own garden/pantry, not the supermarket.
Cross-pillar ties to M: R needs M’s recursion (machine-tool + metrology cells). A only counts mass “at spec”—M is how you reach spec. E quality (harmonics, brownouts) preserves tolerances and FPY. G hosts acceptance authority and calibration pedigree; S sizes spares for critical cells; P feeds the technician pipeline; B depends on validated sterile fabrication.
Lessons Learnt: Automate last; measure first. We learned that metrology is the factory. Before robots, we stabilized tolerances, jigs, heat-treat recipes, and QA. Interchangeability—blind swaps that pass—is the real maturity signal. Variety kills: we cut fastener sizes, stock forms, and finish options until calibration drift and scrap stopped surprising us. Only then did automation pay back instead of scaling defects.
Misjudged Initially:
A hero CNC ≠ capability; without CMM, SPC, and stable fixtures, it’s a sculpture tool.
Underweighted heat-treat and surface processes; specs met on paper, not in property curves.
Treated QA as compliance theater—no FPY or gage R&R meant we were flying blind.
Assumed electronics could be perma-imported; useful-node capability mattered sooner.
Confused “we can print it” with “we can certify it”; AM without post-process and metrology wasn’t production.
Qs to Ask:
What swap-test pass rate do you achieve on your top assemblies?
Which two processes are truly redundant (not just two machines on one line)?
Can you build boards & power discretes at a useful node, and restore CAM/PLM offline within 24 hrs?
Port Harmonia, Mars (Year 94 Mars Human Era)
Here is an example of Port Harmonia’s Manufacturing Breadth MIS in the early third century HE:
M=0.35(0.52)+0.20(0.8)+0.15(0.8)+0.15(0.6)+0.15(0.76)≈0.66
Calculations:
Mcov = 0.52 Coverage: foundations mostly production (0.8), machining 0.8, forming 0.6, surface/heat 0.6, QA/metrology 0.8, electronics (for coverage count) 0.6 → Mcov,raw ≈ 0.69; foundations mean 0.75 ⇒ Mcov ≈ 0.69×0.75 = 0.52
Mtol = 0.52 Precision: IT7 routinely, Ra 0.8 µm, property control 95% ⇒ Mtol ≈ 0.8
Mqa = 0.52 QA: FPY 90%, Gage R&R 85%, Calibration 95%, Interchangeability 90% ⇒ Mqa ≈ 0.8
Melec = 0.52 Electronics: multilayer PCBs + power-electronics assembly ⇒ Melec = 0.6
Muptime = 0.52 Uptime: OEE 75% (0.7), PM 90% (0.8), SMED “<2 h” (0.8) ⇒ Muptime ≈ 0.76
Combine (weights sum to 1)
Suggested simplified weights (disclose if tuned). Coverage/depth is king; precision and QA make parts interchangeable; electronics is a known chokepoint; uptime ensures the capability is operational, not just installed.
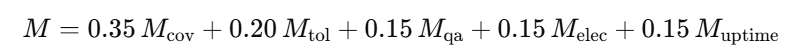
Interpretation:
M < 0.40 — Thin stack; pilot lines and single CNC illusions; minimal metrology.
0.40 – 0.70 — Broad basics; production-grade in key areas; credible QA; limited electronics.
> 0.70 — Deep, redundant processes incl. electronics; robust QA; high uptime; fast reconfig.